7 tips for laser engraving on metal
Metal is notoriously unforgiving under a laser beam. Unlike wood or acrylic, which offer generous room for error, metal dissipates heat rapidly, reflects beams unpredictably, and reacts drastically to slight parameter shifts.
Whether you are personalizing stainless steel drinkware, serializing brass tags, or creating deep relief marks on raw aluminum, here are seven actionable tips to get crisp, professional laser engravings every time.
1. Match the Laser Source to Your Metal Type
Not all lasers interact with metal the same way:
Fiber Lasers (1064 nm): The gold standard for direct bare metal engraving. Their wavelength is readily absorbed by steel, brass, titanium, and aluminum without needing chemical coatings.
MOPA Fiber Lasers: If you want colored marks on titanium or dark, non-oxidized annealing marks on stainless steel, adjustable pulse widths in MOPA systems give you precise thermal control.
Diode & $CO_2$ Lasers: Standard $CO_2$ (10,600 nm) and blue diode lasers (450 nm) reflect right off bare reflective metal or lack the power to etch directly. For these machines, stick to powder-coated tumblers, anodized aluminum (where the laser bleaches the dye layer), or use specialized marking compounds.
2. Degrease and Clean Before Every Run
Machine oils, fingerprints, oxidation, and residual shop dust act as an unintended barrier. When the laser hits an oily smudge, it carbonizes the oil instead of vaporizing the metal, leading to muddy lines and patchy contrast.
Wipe your metal workpiece thoroughly with 90%+ isopropyl alcohol (IPA) or acetone using a lint-free microfiber cloth.
For heavily tarnished brass or copper, run a light brass cleaner first, dry it completely, and finish with an alcohol wipe to remove film residue.
3. Dial in True Focal Distance
Because metal lacks the absorption depth of organic materials, even a fraction of a millimeter off-focus will dramatically dilute power density.
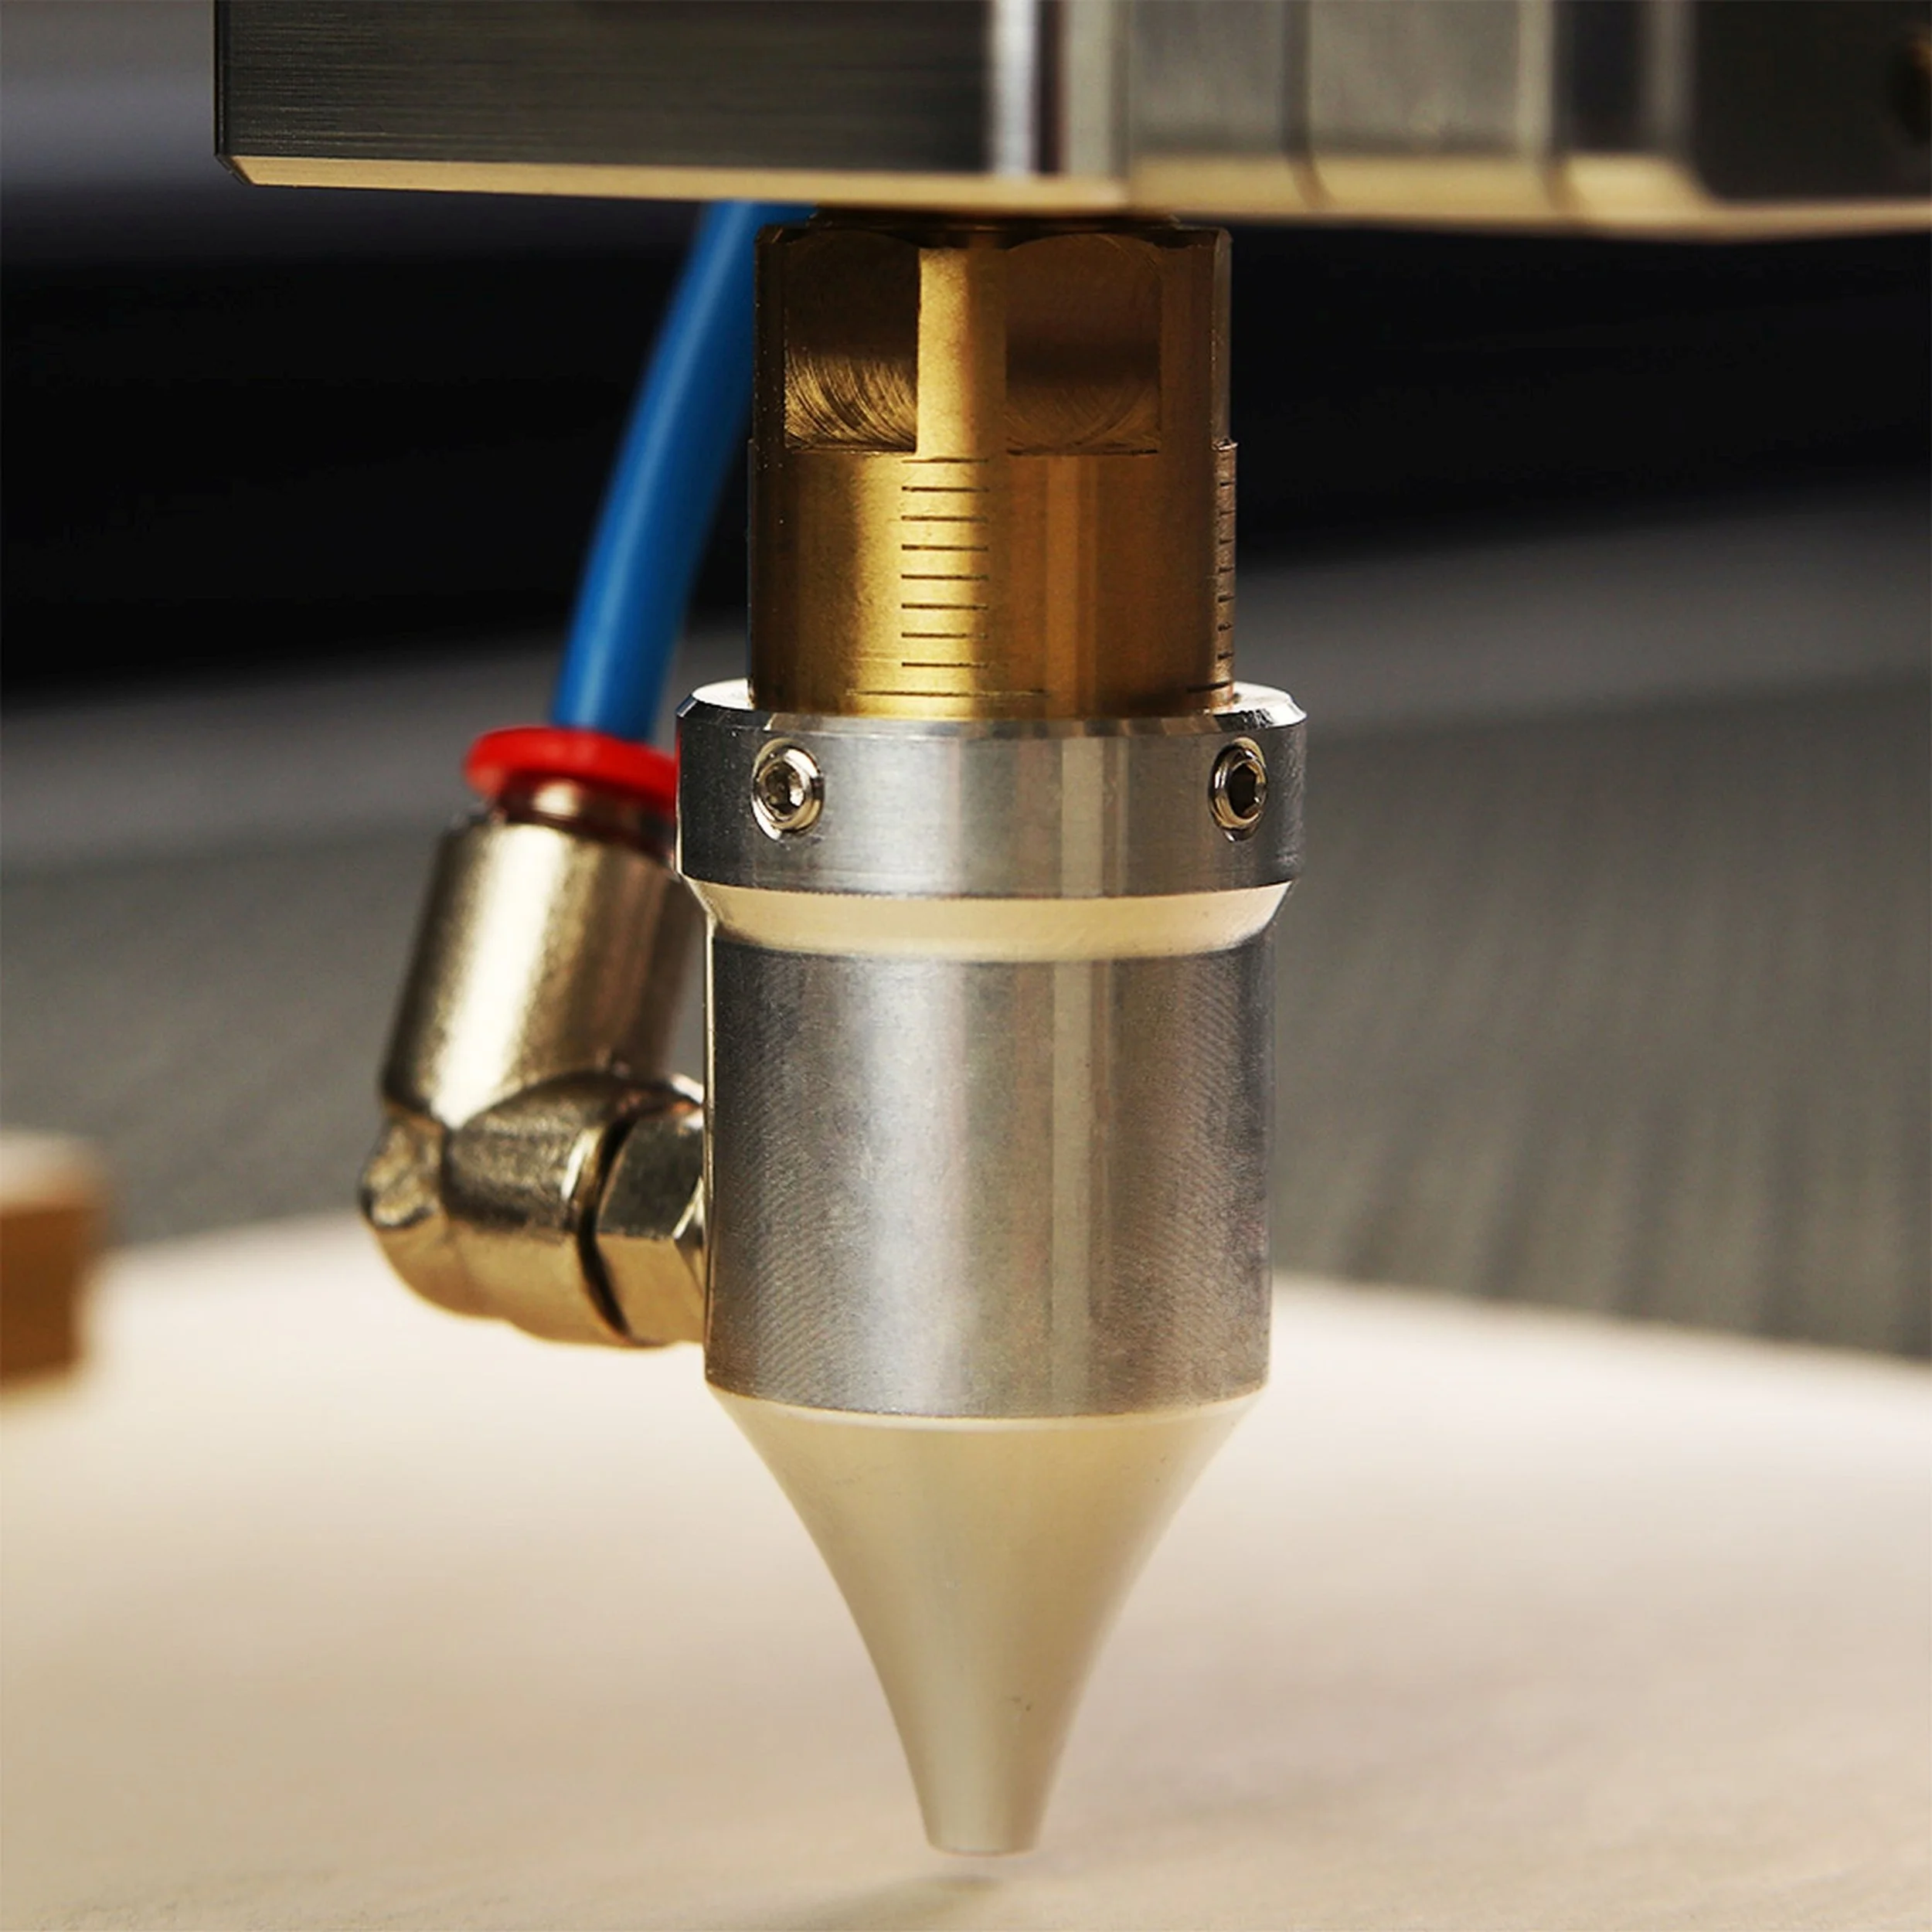
Use your machine’s dual-red-dot focus guides, a stepped focus gauge, or a digital height sensor to calibrate the exact focal plane.
When engraving cylindrical or curved items (like flasks or insulated mugs), always use a dedicated rotary chuck or roller attachment. If the curve falls outside the laser’s depth of field, the edges will quickly blur and lose depth.
4. Optimize Line Interval and Hatch Angles
When filling shapes or letters on metal, the fill pattern—known as hatching—determines surface smoothness:
Hatch Spacing: Setting the line interval too wide leaves visible striations; setting it too tight creates excessive heat buildup. A spacing of 0.02 mm to 0.05 mm is standard for smooth coverage.
Cross-Hatching: For deep engraving, use cross-hatching (e.g., alternating passes at 45° and 135°). Shifting the angle on each pass prevents the laser from carving directional ridges and produces a uniform, flat bottom.
5. Prevent Warping with Smart Heat Management
Metal acts as a heat sink. High-power, slow passes trap thermal energy in the part, causing thin sheets to warp, burr, or discolor around the edges.
Instead of running one slow, scorching pass at 100% power, use multiple passes at higher speeds and moderate power to gradually ablate material while allowing the workpiece to dissipate heat between layers.
For dense geometric fills, break the design into separate layers or use bi-directional marking strategies that spread the thermal load across the object.
6. Safeguard Against Back-Reflection
Highly reflective metals like polished brass, copper, silver, and gold can bounce a 1064 nm beam straight back into the galvanometers or laser aperture, risking permanent optics damage.
Slightly tilt the workpiece by 1° to 2° off direct perpendicular alignment if you suspect dangerous specular reflection.
Ensure your laser source is equipped with an integrated optical isolator to safely absorb back-reflected photons.
7. Run a Parameter Matrix on Identical Scrap First
Factory setting presets are starting points, not final answers. Material grade matters: 304 stainless reacts differently than 316, and 6061 billet aluminum engraves differently than cast aluminum.
Keep cut-offs or blank swatches of your exact project alloy.
Burn a test matrix grid varying speed on one axis and power or frequency on the other. This visual map helps you instantly spot the exact threshold where clean ablation occurs without scorching.
Contact Us
Let White Dog Engraving save you the time, money and hasssle of lase engraving! Contact us today by clicking here to get a quote.